EN
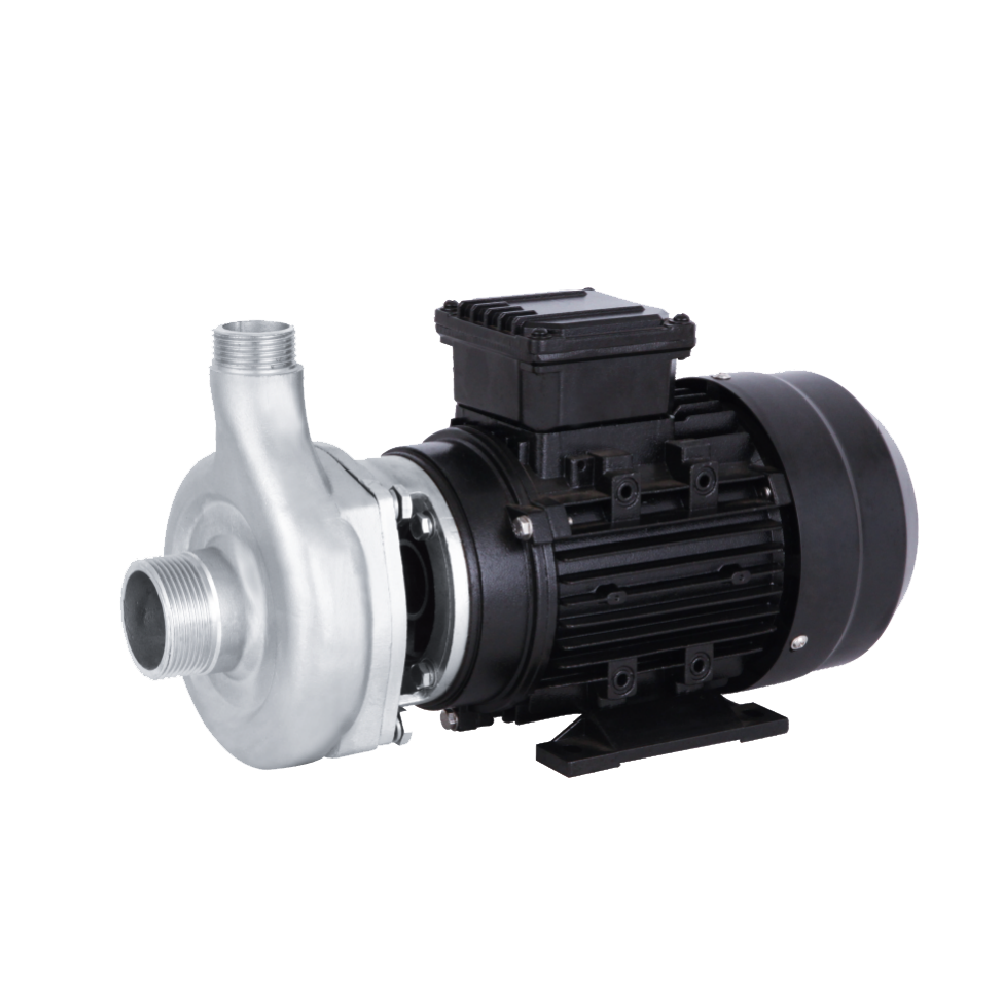
WB(D)S Stainless Steel Anti-Corrosion Centrifugal Pump for Chemical Liquid Transfer
This stainless steel anti-corrosion centrifugal pump is designed for acid, alkali, and chemical liquid transfer applications, providing reliable corrosion resistance, stable water flow, and efficient performance for industrial pumping systems.
- Overview
- Specificatons
- FAQ
- Recommended Products
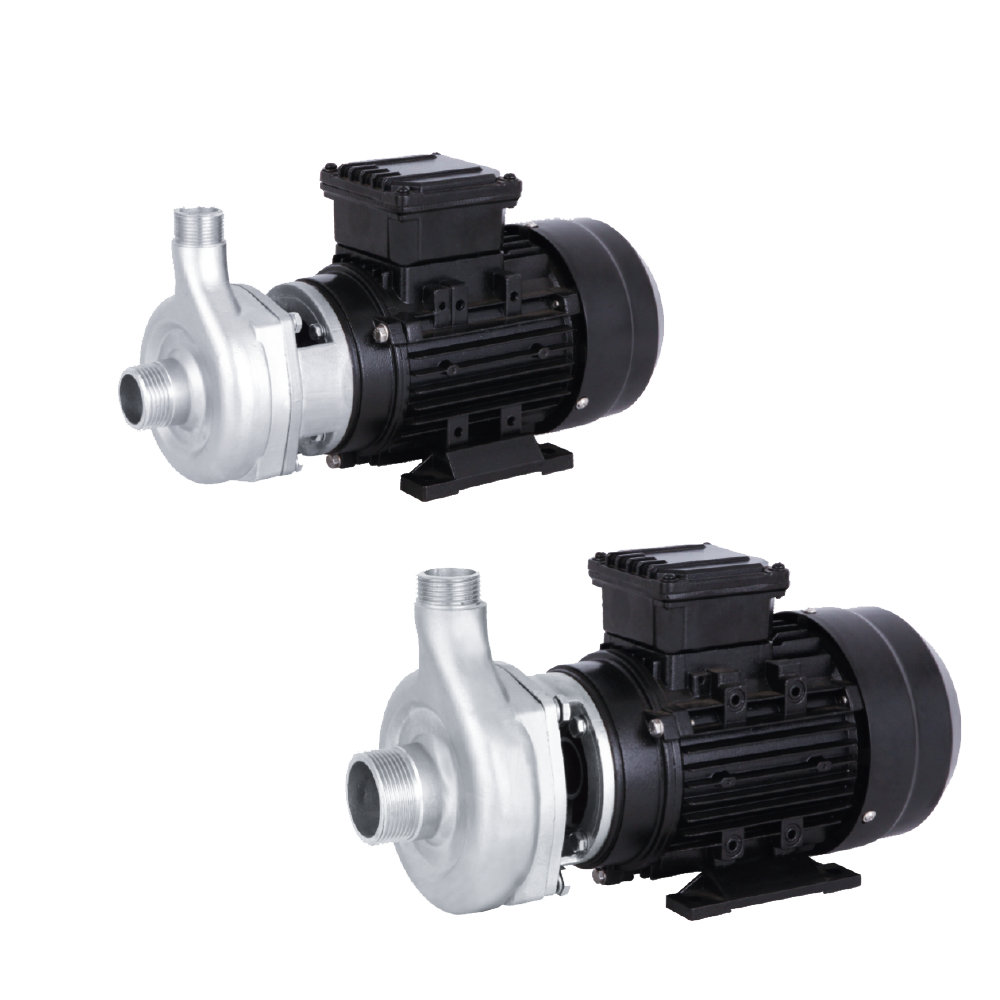
The stainless steel anti-corrosion centrifugal pump is an engineered, heavy-duty fluid management solution designed specifically for transferring highly corrosive liquids, aggressive chemicals, volatile industrial fluids, and processed effluents. Operating via an advanced close-coupled or frame-mounted drive alignment, this high-performance anti-corrosion centrifugal pump safely handles strong acids, alkalis, chemical solutions, electroplating bath liquids, and deionized water networks without structural degradation. By combining specialized internal hydraulics with non-reactive surface finishes, this industrial-grade chemical transfer pump prevents hazardous fluid leaks, eliminates pipeline contamination risks, and maintains a completely smooth liquid flow trajectory across complex chemical processing systems.
Manufactured with high-quality stainless steel materials—such as premium-grade SUS304 or optional SUS316L alloys—this durable stainless steel anti-corrosion centrifugal pump offers excellent corrosion resistance, reliable mechanical operation, and an extended service life in demanding chemical environments. Featuring a computer-optimized centrifugal impeller system and stable hydraulic performance characteristics, the pump delivers high-efficiency volumetric discharge, uniform fluid velocity, and low-vibration execution during continuous-duty running cycles. Its rugged casing architecture makes it an ideal choice for critical industrial projects requiring safe, cost-effective, and absolutely reliable chemical fluid handling.
Main Advantages & Value Proposition
Investing in our stainless steel anti-corrosion centrifugal pump delivers immediate technical and operational advantages for heavy industrial facilities and fluid infrastructure:
Excellent Corrosion & Acid Resistance: Premium stainless steel construction protects the inner flow paths from pitting, erosion, and chemical degradation caused by industrial acids and alkaline washes.
High-Efficiency Volumetric Delivery: The hydrodynamically balanced centrifugal impeller converts motor torque into fluid velocity with minimal internal friction losses.
Low Vibration & Quiet Operation: High-precision manufacturing ensures rigid shaft alignment, which reduces mechanical noise and extends bearing life during continuous cycles.
Leak-Proof Mechanical Sealing: Fitted with high-end chemical-grade mechanical seals, protecting personnel and the environment from hazardous chemical fluid leaks.
Continuous-Duty Industrial Build: Engineered for uninterrupted 24/7 industrial execution, minimizing maintenance overhead and preventing costly production line shutdowns.
Advanced Manufacturing Craftsmanship & Structural Features
At our specialized production facility, each stainless steel anti-corrosion centrifugal pump is engineered utilizing high-precision CNC machining centers and automated metallurgical diagnostic stations:
⚙️ Precision Investment-Cast SUS304/SUS316L Volute
The liquid-end casing of our anti-corrosion centrifugal pump is created using advanced investment casting techniques. This creates smooth internal walls that eliminate hydraulic friction, maximize velocity, and prevent chemical scaling or salt accumulation over time.
100% Pure Copper-Wound Industrial Motor
The drive core features 100% pure copper wire windings wrapped in high-temperature enamel insulation. This layout guarantees that the chemical transfer pump maintains optimal energy efficiency, reduces electrical resistance, and prevents premature motor insulation breakdown under high thermal operating loads.
Strict Quality Standards & Professional B2B Service
As an established global manufacturer and exporter of stainless steel anti-corrosion centrifugal pumps, our operations are anchored by rigorous international quality assurance metrics.
[Mandatory B2B Factory Inspection Protocol]
Raw Stainless Material Assay -> Impeller Dynamic Balance -> Hydrostatic Pressure Leak Test -> 100% Flow Performance Charting
Every single stainless steel anti-corrosion centrifugal pump undergoes a mandatory 100% automated pressure, electrical insulation, and sealing validation before export boxing, ensuring defect-free field reliability from the moment it arrives at your construction site.
Strategic OEM & ODM Batch Customization:
Metallurgical Upgrades: Upgrading all fluid-contact components to SUS316L or titanium alloy for extreme salt spray, marine, or ultra-high temperature acid processing lines.
Motor Enhancements: Equipping the pump with specialized ATEX-certified explosion-proof motors for environments handling volatile chemical solutions or solvents.
Flange & Inlet Standard Matching: Precision machining of intake and discharge flanges to seamlessly match your regional ANSI, DIN, or JIS piping layouts.
Versatile Application Scenarios
The non-reactive handling capabilities of the stainless steel anti-corrosion centrifugal pump make it a core asset across multiple commercial, chemical, and municipal water infrastructures:
A. Chemical Processing Plants & Refineries
Regulates the transport, loading, and mixing of raw chemical acids, alkalis, saline mixtures, and intermediate chemical solutions throughout the production grid.
B. Industrial Water Treatment & Electroplating
Cycles aggressive plating chemicals, acid baths, and corrosive rinsing solutions in electroplating facilities, and manages chemical dosing in wastewater treatment installations.
C. Acid & Alkali Circulation Systems
Ideal for closed-loop industrial circulation setups, clean-in-place (CIP) wash networks in food plants, and chemical liquid transfer projects worldwide.
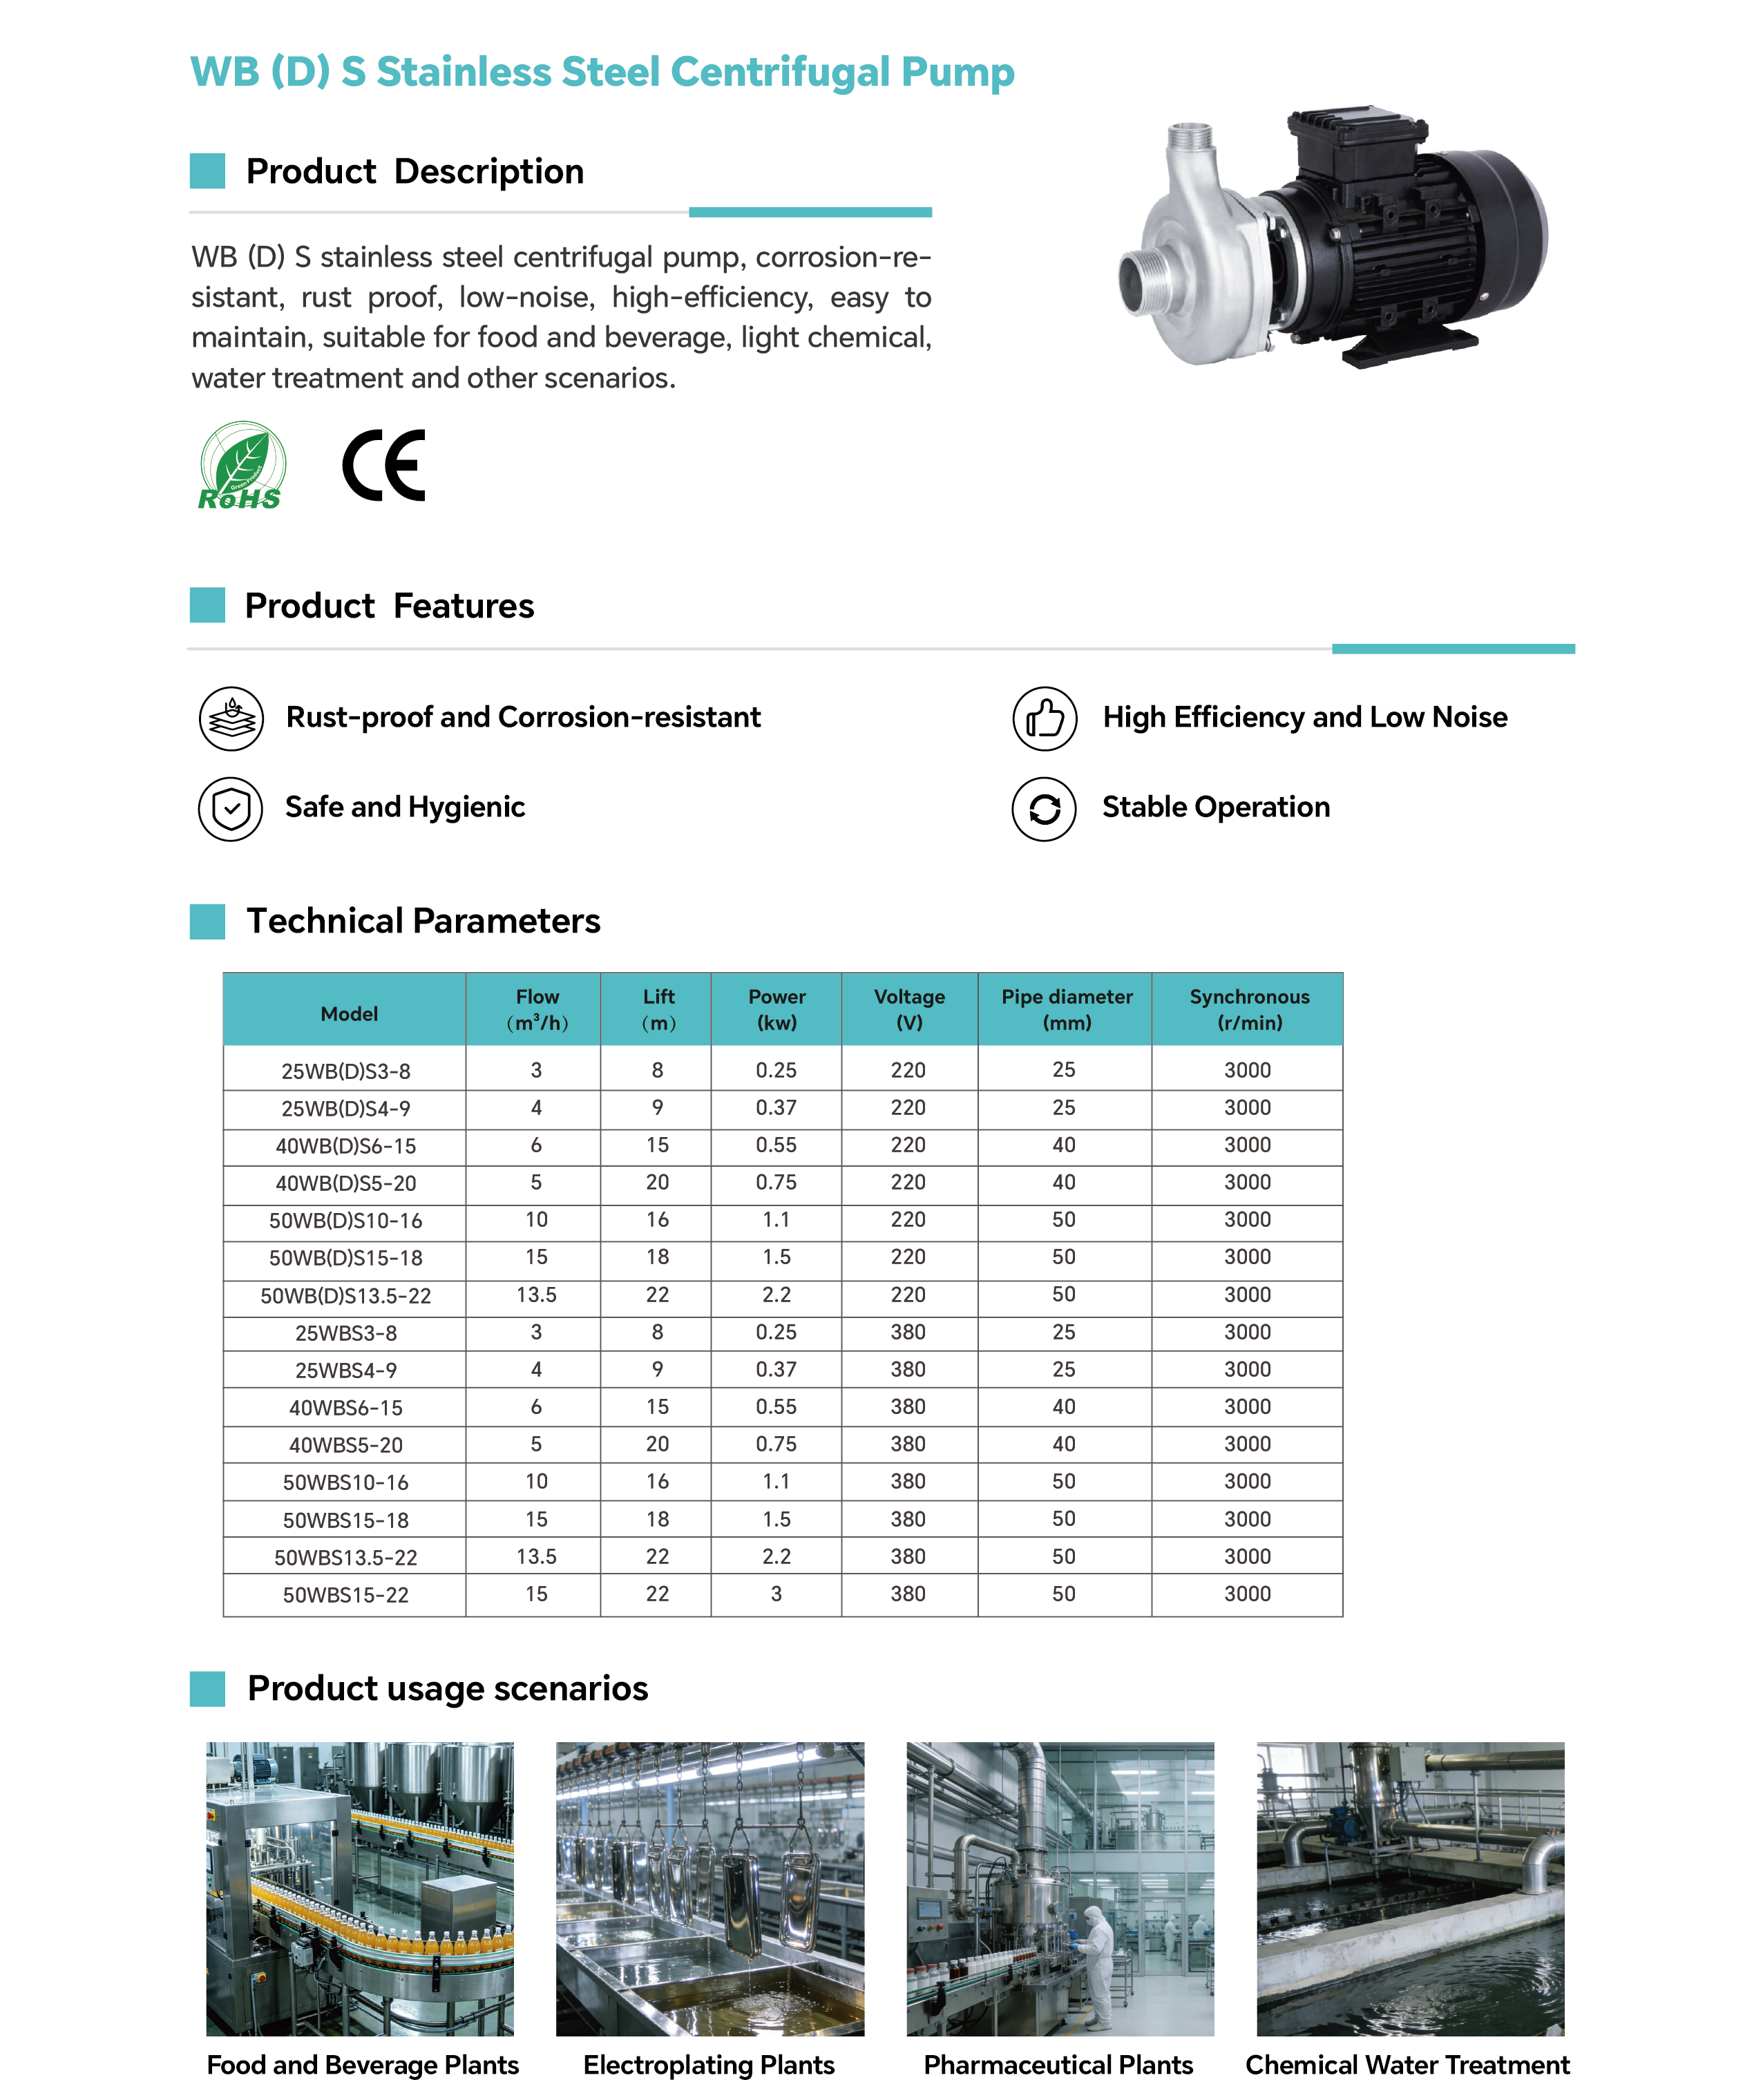
To facilitate seamless engineering evaluation and international B2B procurement selection, the core technical specifications for our standard stainless steel anti-corrosion centrifugal pump configurations are detailed below:
| Technical Parameter | Specification & Customizable Range |
| Product Model | SSC-Chemical Corrosion-Proof Series |
| Pump Classification | Stainless Steel Anti-Corrosion Centrifugal Pump |
| Primary Metallurgy | Premium SUS304 Stainless Steel |
| Shaft Sealing Type | Specialized Chemical-Resistant PTFE Mechanical Seal / Viton O-Rings |
| Motor Winding Core | 100% Pure Copper Wire Motor with Class F Thermal Insulation |
| Voltage & Grid Frequency | 380V (Three-Phase, 50Hz / 60Hz Adaptive) |
| Inlet / Outlet Diameters | 1.5 inch, 2 inch, up to 3 inch Flanged Connections (ANSI / DIN Standards) |
| Max Volumetric Flow Rate | Up to 10 m³/h - 15 m³/h (Depending on specific model power) |
| Max Lift Head Capabilities | Up to 8 - 22 meters vertical dynamic head |
Q1: Is this chemical transfer pump self-priming or does it require flooded suction?
A: This standard centrifugal series requires a flooded suction (the liquid source must be higher than the pump intake) or the installation of a foot valve to ensure the internal volute is primed with liquid before starting the motor.
Q2: Do you support custom voltages for international industrial distribution networks?
A: Yes, absolutely! As a professional factory, we provide full OEM support. We can custom configure the motor of your stainless steel anti-corrosion centrifugal pump to match three-phase 220V, 380V, 415V, or 440V at either 50Hz or 60Hz grid frequencies depending on your regional marketplace requirements.
Conclusion & B2B Inquiry Call to Action
The stainless steel anti-corrosion centrifugal pump represents the ultimate combination of non-reactive hydraulic centrifugal engineering, stable mechanical torque, and long-lasting SUS304/316L chemical durability. For global industrial wholesale machinery distributors, chemical plant engineering contractors, water treatment system builders, or regional procurement consultants seeking factory-direct pricing on premium industrial chemical pumps, this series stands out as an incredibly dependable, high-performance asset.
Contact Our Export Engineering Division:
Ready to receive a competitive, factory-direct bulk quotation or discuss custom OEM batch manufacturing details? Reach out directly to our international trade department via WhatsApp or Email. We provide quick-response technical consulting, accurate maritime freight calculations, and comprehensive after-sales technical backing.
📞 Business WhatsApp / Phone: +86 180 0586 6139
🌐 Manufacturing Entity: Larissa Pump